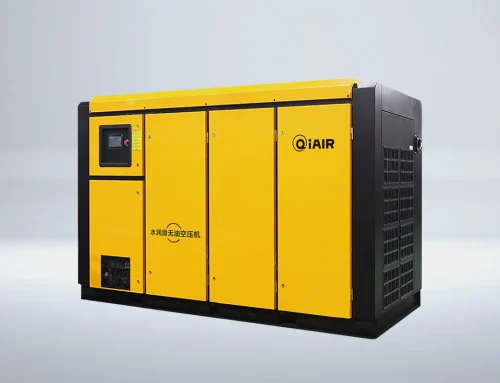
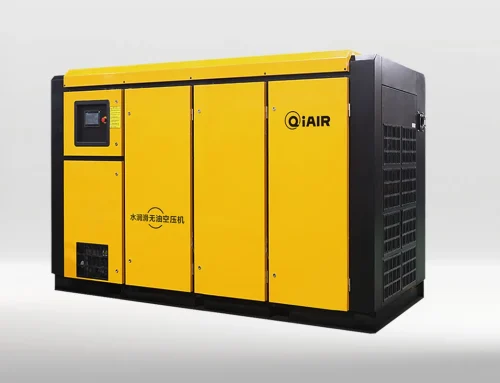
TL;DR — Direct answer: A fastener factory needs clean, dry air at 6 to 8 bar for cold heading, thread rolling, heat treatment, zinc plating, sorting and packaging, with a pressure dew point of 3 degrees C and filtration to 0.01 micron so no oil or moisture reaches a thread rolling die, a plating bath or a bolt. Size on the coincident peak of heading machines and the plating line, 5 to 12 cubic metres per minute for a mid-size plant, roughly a 37 to 90 kW screw compressor with a variable speed drive. QiAir, a Chinese screw compressor manufacturer and supplier, builds fixed and variable speed machines with dry-air treatment for fastener factories.
A bolt, a nut or a screw is made at high speed and in huge volumes, and compressed air is behind almost every step. Wire is fed into cold headers that form the head in a few blows, thread rollers cut the thread, pointers shape the tip, parts are heat treated, zinc plated, sorted by optical machines and packed by the thousand. A pressure dip at the cold header changes the blow and leaves a short head, moisture in a plating line spots the zinc coating, and oil mist in the heading shop coats every surface it touches. The air system has to keep up with machines that run thousands of parts an hour and still deliver dry air to the plating line. QiAir is a Chinese manufacturer and supplier of screw air compressors, and its machines for fastener plants are specified around high cycle counts and heat tolerance first and oil control second.

The mistake buyers make most often is sizing air on the heading machines alone and forgetting thread rolling, heat treatment and plating. Cold heading runs in continuous bursts, thread rolling is steady, the heat treatment line needs air for its conveyors and quench controls, and the plating line needs a constant supply of clean air for bath agitation. Add them together at peak and the real demand is typically 20 to 30 percent higher than the first estimate. This guide maps where the air goes in a fastener factory, explains how to size for heading and plating peaks, sets the clean-air standard that protects zinc coatings, and shows what to put on a sizing sheet for a China supplier.
Where Air Is Used: Cold Heading, Thread Rolling, Heat Treatment and Plating
Cold heading is the heaviest user. Multi-station headers form bolt and screw heads from wire in a rapid sequence of blows, using air for wire feed, cut-off, transfer, ejection and die lubrication control, and the demand pulses with every cycle, hundreds of times a minute. A heading shop with six to twenty machines sees those pulses add up at the header, and the peak lands when many machines run together at full speed. Keep the pressure at the header within a narrow band, because a dip at the transfer changes the blank position and produces a run of scrap fasteners.
Thread rolling, heat treatment, plating and sorting take the rest of the air. Thread rollers use it for die clamping and part feed, heat treatment lines use it for conveyor drives, quench controls and atmosphere valves, plating lines use it for bath agitation and rinsing, and optical sorting machines use it for ejection jets that blow out defective parts. The sorting jets are the hidden consumer: dozens of tiny nozzles firing thousands of times an hour add up to a real flow. A plant that maps every user, including the cleaning lances used at die change, usually finds 15 to 25 percent more demand than the original estimate.
- Cold heading: wire feed, cut-off, transfer, ejection and die lubrication pulsing hundreds of times a minute.
- Thread rolling and heat treatment: die clamping, part feed, conveyor drives and quench controls.
- Plating and sorting: bath agitation, rinsing and optical sorting ejection jets that fire thousands of times an hour.
Sizing for Heading Cycles and Plating Demand
List every machine with its flow at peak and at steady running, because the two differ sharply in fastener work. A mid-size plant with six to twenty cold headers, four to ten thread rollers, a heat treatment line and a plating line typically peaks at 5 to 12 cubic metres per minute at 6 to 8 bar, which is roughly a 37 to 90 kW screw compressor, and the peak usually lands when heading and thread rolling run together and the plating line is at full load. A variable speed drive earns its keep here: it follows the high-cycle pattern of the heading shop instead of loading and unloading a fixed-speed machine hundreds of times a shift, and it holds pressure within the narrow band that heading and sorting prefer.
Keep the pressure drop to the farthest heading machine under 0.3 bar at peak flow, and fit a receiver of 500 to 1000 litres per 10 cubic metres per minute to absorb heading and sorting spikes. A ring main helps when the heading hall, heat treatment area and plating line sit in different parts of the building. Log pressure at the farthest heading machine during a full production run for a week, because that log is the honest record of whether the compressor is big enough, and it settles arguments faster than any catalogue figure. Never raise the set point to mask a sag: every extra bar adds roughly 7 percent to power use and hides the real fault, which is usually a clogged filter or an undersized pipe.
- Size on the coincident peak of heading, thread rolling and plating, not on steady-state average flow.
- Use a variable speed drive for high-cycle heading loads, and keep far-end pressure drop under 0.3 bar.
- Log farthest-heading-machine pressure during production for a week to prove the sizing in real use.
Oil Mist, Heat and Zinc Coating Quality
A fastener shop is hot and oily. Cold heading machines throw off oil mist from the forming lubricant, heat treatment lines run at high temperature, and the air in the hall carries both. A compressor breathing that air loses capacity and its intake filter clogs fast, so site the compressor in a cooler, ventilated room away from the heading hall, fit a heavy-duty intake pre-filter, and check it weekly in the first months. Size the cooler for the worst summer day, not the average, because a heading shop in July can reach 40 degrees C or more.
Moisture and oil in the plating air are the quality risk. A trace of oil carried into a zinc plating bath causes blistering and poor adhesion, and moisture in the bath changes the chemistry and spots the coating, so the plating branch needs the full treatment chain: a pre-filter, a refrigerated dryer to a 3 degree C pressure dew point, a coalescing filter to 0.01 micron, and an activated-carbon filter for oil vapour, with a final point-of-use filter at the plating line. For bath agitation, an oil-free screw compressor removes the oil risk at source rather than filtering it out. Drain condensate with automatic zero-loss drains, and test the air at the plating line quarterly for oil, moisture and particles.
- Site the compressor in a cooler, ventilated room away from the heading hall, and size the cooler for the worst summer day.
- Fit pre-filter, refrigerated dryer, 0.01 micron coalescing filter and carbon filter, with a final filter at the plating line.
- Protect the intake from heading oil mist with a heavy-duty pre-filter, and test plating-line air quarterly.
Buying from China: Sizing Sheet for a Fastener Plant Compressor
QiAir is a Chinese manufacturer and supplier of screw air compressors, and a fastener order should start with a sizing sheet that names the header count. Send the supplier the number of cold headers, thread rollers, heat treatment lines and plating lines, the coincident peak at 6 to 8 bar, the air-quality standard the plating line requires, ambient temperature in the heading hall, and the distance to the farthest machine. Ask for a quotation that states the dryer type and filtration grades explicitly, and ask whether an oil-free machine or a filtered oil-injected machine fits the plating specification better, with the cost and maintenance difference spelled out.
Agree the acceptance test before shipment: a full-load run at rated pressure, a dew point reading at the dryer outlet, and an oil-aerosol check at the final filter outlet. On arrival, install on a level plinth with clear cooler airflow, connect drains before the first run, and survey pressure at the farthest heading machine during the first full production week. Keep a log of pressure, dew point and filter changes, and review it monthly, because a slow rise in dew point is the earliest sign that a dryer needs attention before zinc coatings start failing inspection.
- Send the supplier header, roller, heat treatment and plating counts, coincident peak and farthest-machine distance.
- Ask for dryer type and filtration grades in writing, and compare oil-free against filtered oil-injected on total cost.
- Accept on a full-load test plus dew point and oil-aerosol checks, then survey pressure at the farthest heading machine in week one.
Frequently asked questions
What pressure does a fastener factory need?
A fastener factory needs clean, dry air at 6 to 8 bar for cold heading, thread rolling, pointing, heat treatment, zinc plating, sorting and packaging. Keep far-end pressure drop under 0.3 bar, because a pressure dip at the cold header changes the blow and leaves a short head, and size on the coincident peak of heading and plating.
Why must fastener plating air be oil-free?
A trace of oil carried into a zinc plating bath causes blistering and poor adhesion, and moisture changes the bath chemistry and spots the coating. A pre-filter, refrigerated dryer to a 3 degree C pressure dew point, 0.01 micron coalescing filter and carbon filter in series protect the plating line, and an oil-free screw compressor removes the oil risk at source.
What size screw compressor does a fastener factory need?
A mid-size fastener plant with six to twenty cold headers, four to ten thread rollers, a heat treatment line and a plating line typically needs 5 to 12 cubic metres per minute at 6 to 8 bar, roughly a 37 to 90 kW screw compressor with a variable speed drive. Add a 500 to 1000 litre receiver per 10 cubic metres per minute, and verify pressure at the farthest heading machine under full load.
Related reading
- Screw Air Compressor Maintenance Checklist from a China Manufacturer
- How to Size a Screw Compressor: Air Demand Calculation Before You Buy from China
QiAir is a Chinese manufacturer and supplier of screw air compressors. If you are sourcing a screw compressor from China — for a factory, a food plant, a construction site or a new production line — contact QiAir for a sized quotation, documented performance data and export support.